 Search


 English
 中文简体
 русский
 عربى



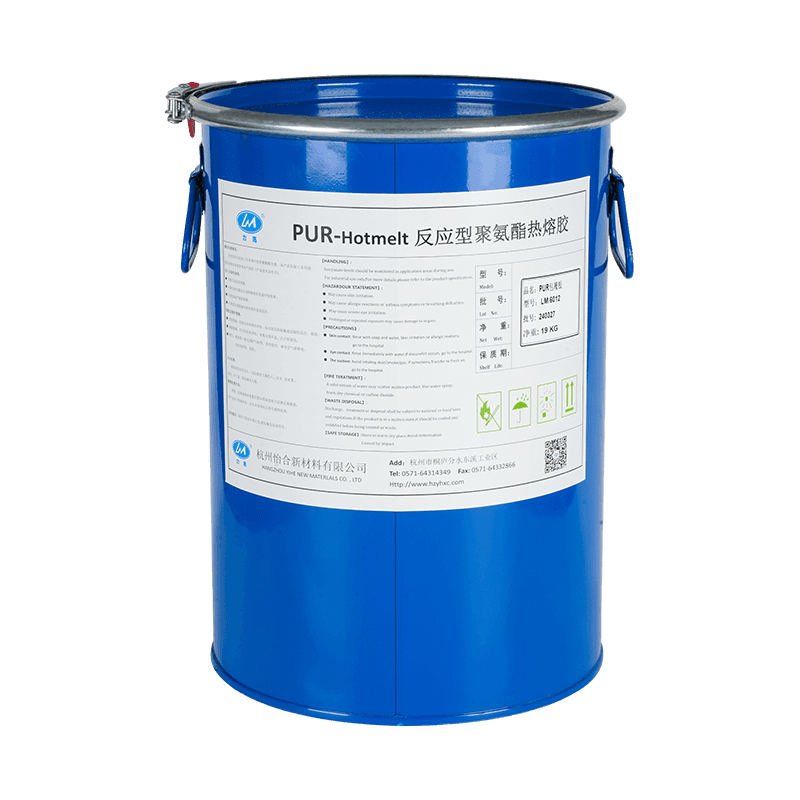





Hangzhou Yihe New Materials Co., Ltd. has been formulating adhesives at our Tonglu site in Hangzhou, China since 1997. Within our PUR Hot Melt Adhesive manufacturer range we supply one-component reactive polyurethane systems for flat lamination, profile wrapping, edgebanding and cold-press assembly — solvent-free products that build bond strength by reacting with ambient moisture rather than by drying.
The range is built for furniture, cabinetry, interior doors, wall panels and other wood-based production where a joint has to survive heat, humidity and years of handling. Each grade is matched to the way the adhesive is applied and to the materials on either side of the glue line, not simply to a generic category.
The PUR range at a glance
| Product family | Form and cure | Typical process | Facing and substrate fit |
|---|---|---|---|
| PUR Flat Lamination Hot Melt Adhesive (LM6016) | 100% solids, moisture-curing hot melt | Roller, slot-die or curtain application with panel press | Veneer, laminate, CPL and decorative films onto MDF, plywood and particleboard |
| PUR Wrapping Hot Melt Adhesive (LM6012) | Solvent-free, one-component reactive hot melt | Profile wrapping lines with hot melt applicator and pressure rollers | PVC, paper and foil wrap over MDF, chipboard and engineered profiles |
| PUR Edgebanding Hot Melt Adhesive (LM6019) | 100% solids, moisture-curing hot melt | Automatic and manual edgebanders, straight and shaped edges | PVC, PU paper and comparable edgebanding films onto board and door blanks |
| Liquid PUR Adhesive (LM2260) | Solvent-free reactive liquid, moisture-curing | Cold press, roller or spreader application, assembly bonding | Panel-to-panel lamination, veneered faces and general assembly joints |
Application fit across the four production points
Flat lamination of large panels
LM6016 PUR Moisture-Curing Hot Melt Adhesive is formulated for wide-area bonding, where the adhesive has to stay uniform from the leading edge to the trailing edge of a full-size panel. The working point is set so the film still wets the facing when the press closes, then develops handling strength quickly enough for the panel to move down the line.
Profile wrapping and radius coverage
LM6012 General PUR Wrapping Hot Melt Adhesive is aimed at wrapping lines where melt flow, open time and roller pressure decide whether a wrap stays tight on a radius. It suits wood chips, engineered board and machined profiles finished with PVC, paper or foil, and it is applied hot with a short, controlled gap before the wrapping roller closes the joint.
Edgebanding on doors and furniture boards
LM6019 General PUR Edgebanding Hot Melt Adhesive bonds PVC, PU paper and similar edgebanding films to board and door blanks on both automatic and manual machines. The reactive bond is chosen where an edge faces heat, moisture and abrasion in service and where a visible glue line would show through a thin band.
Cold press and liquid PUR assembly
The Liquid PUR Adhesive family covers cold-press lamination and assembly work, where a reactive liquid is spread on the substrate and the stack is closed under pressure before curing continues in the joint. It is the practical route for plants without a hot melt melter, or for assemblies that need a longer lay-down window than a hot melt allows.
Substrate and workpiece considerations
The same PUR grade can behave differently on two boards that look identical on a sample rack. We look at the following before naming a product:
- Surface density and porosity — machined MDF, chipboard and plywood draw adhesive away from the glue line at different rates, which shifts coat weight and press time.
- Moisture content of the wood — reactive PUR uses ambient and substrate moisture to cure; boards that are too dry or too wet change both green strength and final cure.
- Facing chemistry — high-gloss PVC and skin-feel films can carry plasticizer that migrates into an adhesive layer, so the facing is checked together with the grade.
- Edge geometry — band thickness, radius, and whether the edge is straight or shaped determine how much adhesive stays in the joint after trimming.
- Panel temperature — a cold panel in a winter workshop shortens the usable assembly window even when the melter is at the correct setting.
Line integration, curing and process control
Reactive PUR is applied hot and cures by reaction, so the machine settings and the workshop conditions both belong to the specification. The settings below are established with you on the actual line rather than taken from a generic table:
- Melter and hose temperature — set inside the working window of the grade, with the applicator head checked as well as the tank.
- Coat weight — measured on your substrate and facing combination; heavier is not stronger once the film stops transmitting moisture.
- Open time against line speed — the gap between application and press closure must stay inside the assembly window of the grade.
- Press pressure and dwell — enough contact to wet the full bond area without starving the joint on shaped profiles.
- Humidity and airflow — curing needs moisture; very dry or very cold rooms slow the reaction and delay downstream machining.
- Cleanout and purging — moisture-curing adhesive left hot in a tank or on a roller will skin and set; shutdown routines are agreed with the operators before the first production run.
Quality assurance from raw material to batch
Hangzhou Yihe New Materials holds National High-Tech Enterprise qualification and operates under ISO 9001 quality management and ISO 14001 environmental management certification. Incoming raw materials are tested before production, and each batch is traceable from the drum or pail back to its production record.
Trial acceptance is agreed before scale-up, so both sides know what a pass looks like:
- Bond strength and peel behaviour on the actual board and facing, tested after conditioning rather than straight off the press.
- Heat and moisture resistance on finished edges, wraps and laminated faces, using the conditions your product will meet in service.
- Visual criteria — glue line, surface haze, telegraphing through thin films, and cleanliness after trimming.
- Batch documentation, including technical data sheet, safety data sheet and certificate of analysis for the delivered lot.
Customization, trials and technical support
Our laboratory and R&D team work within the reactive PUR platform to adjust a grade for a specific substrate, climate or line speed when the standard product does not land on the working point. That work starts with a sample trial in Tonglu and continues with an on-line trial at your plant, where the settings are transferred to your operators and confirmed on production output.
Support covers melter start-up guidance, coating checks, cure and conditioning advice, and troubleshooting when a bond shows haze, edge lift or slow strength development. Distributors receive the same technical material and can call on our team when a customer changes board supplier or facing film.
Documentation, packaging and delivery scope
Every order is accompanied by the current technical data sheet, safety data sheet and batch certificate of analysis. Storage and handling instructions travel with the goods so that warehouse staff and line operators work from the same sheet.
Container format is confirmed against your melter size, consumption rate and warehouse conditions, and the delivery scope is stated in the quotation: product, documentation, sample quantity and any agreed on-site support. Sealed containers, dry storage and stock rotation remain part of the handling agreement, since moisture-curing adhesive will skin if a container is left open.
Information we use to configure your solution
| Project input | Why it decides the recommendation |
|---|---|
| Substrate type, density and moisture content | Sets absorption, coat weight and cure behaviour |
| Facing or edgebanding material, thickness and finish | Determines wetting, plasticizer risk and glue-line appearance |
| Line type, applicator, melter and line speed | Matches open time, melt flow and application method |
| Press pressure, dwell and downstream handling time | Confirms green strength against the production rhythm |
| Service conditions: heat, humidity, interior or exterior use | Sets the durability target used in acceptance testing |
| Workshop temperature and humidity range through the year | Affects cure speed and the practical assembly window |
| Consumption rate, container preference and delivery destination | Shapes pack size, stock rotation and shipping documents |
| Required test methods and compliance documents | Defines the trial report and paperwork issued with the offer |
Frequently asked questions
Which PUR product fits flat lamination rather than wrapping or edgebanding?
Flat lamination uses LM6016, which is designed for wide-area bonding of veneer, laminate and decorative film onto panels. Wrapping uses LM6012, where melt flow and short assembly time matter on a radius. Edgebanding uses LM6019, where the joint is narrow and the finished edge must resist heat and wear.
Does reactive PUR suit interior doors and wet or humid service?
The reactive polyurethane bond is chosen for exactly those conditions, because it resists heat and moisture better than a thermoplastic hot melt. The grade, coat weight and cure schedule still have to be matched to the door construction, so we confirm performance on your board and edge material before release.
Can you match an adhesive we already run on our line?
Send the current technical data sheet, the substrates and the line settings, and our laboratory will work towards an equivalent within the reactive PUR platform. A sample trial in Tonglu is followed by an on-line trial so that the match is proven on your equipment, not only in a beaker.
How is the adhesive supplied and stored?
Products ship in sealed containers sized to the melter and consumption pattern agreed in the quotation, with technical and safety documentation for each batch. Storage must be dry and within the temperature range on the data sheet, and containers should be resealed after use because moisture-curing adhesive skins on contact with air.
Do you support both automatic and manual application?
Yes. LM6019 is used on automatic edgebanders and manual machines, and the liquid PUR range covers cold-press and spreader application where no melter is installed. Our team reviews the applicator, the settings and the operator routine during the trial run.
What is the starting point for a quotation?
A quotation is prepared from the substrate, facing or edgebanding material, line type and speed, workshop conditions, consumption rate and required test documentation. With those details, we propose a grade, a trial plan and a supply format rather than a price against a product name alone.











